


Description
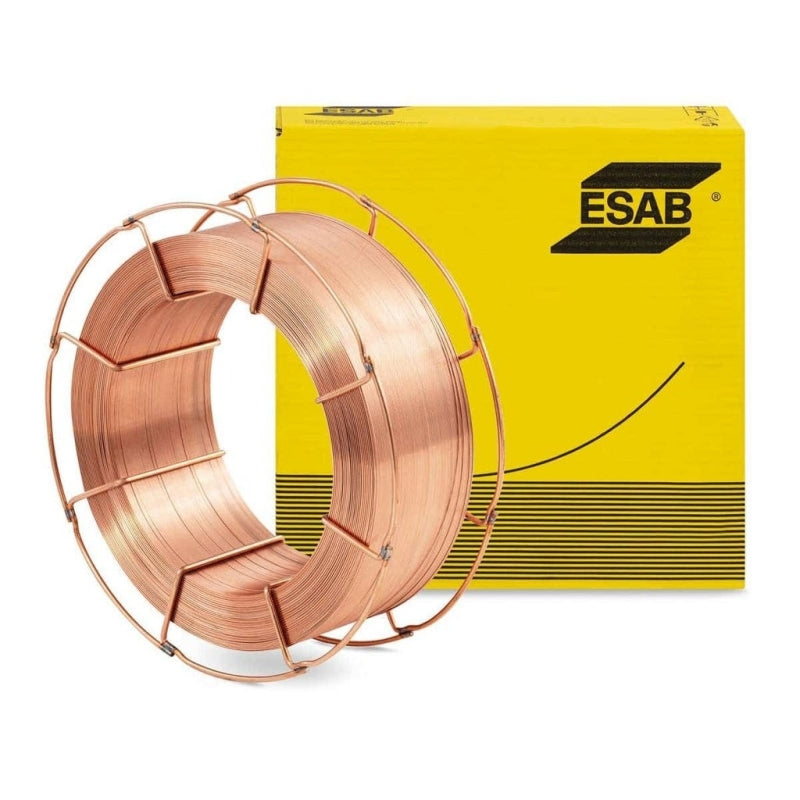
ESAB AUTROD 12.51 MIG wire: the mild steel solid wire for MIG/MAG welding
The ESAB AUTROD 12.51 MIG wire is a mild steel solid wire designed for MIG/MAG welding on non-alloy and low-alloy steels. It ensures a stable arc, low spatter, and clean welds.
Manufactured by ESAB, a global leader in welding, this wire meets the requirements of industrial applications as well as maintenance tasks.
Available at Dagobert Industrie, it fits your standard spools for immediate implementation.
Presentation of the ESAB AUTROD 12.51 MIG wire
The ESAB AUTROD 12.51 is a mild steel solid wire designed for MIG/MAG welding. It is intended for common applications on non-alloy and low-alloy steels, both in the workshop and on-site.
This wire is manufactured by ESAB, one of the world leaders in welding. It benefits from a meticulously copper-coated surface that ensures smooth feeding and good electrical conductivity at the contact tip.
Result: a stable arc, low spatter, and clean beads even at high speeds.
Composition and normative classification
AUTROD 12.51 is classified as G3Si1 according to EN ISO 14341-A, which corresponds to the ER70S-6 designation according to AWS A5.18. This is the reference classification for mild steel MIG wires.
Its composition includes high levels of silicon (Si) and manganese (Mn), which act as powerful deoxidizers. This allows welding of slightly rusted or mill-scaled steels without compromising the quality of the joint.
The recommended shielding gases are Ar/CO₂ mixtures (typically M21) or pure CO₂. The choice of gas directly influences penetration and bead appearance.
| Wire | Classification EN ISO 14341-A | Equivalent AWS | Si Content | Typical Usage |
|---|---|---|---|---|
| ESAB AUTROD 12.51 | G3Si1 | ER70S-6 | ~0.90 % | Mild steel, imperfect surfaces |
| ESAB AUTROD 12.10 | G2Si1 | ER70S-3 | ~0.65 % | Mild steel, clean surfaces |
| Lincoln Electric SuperArc L-56 | G3Si1 | ER70S-6 | ~0.85 % | Mild steel, imperfect surfaces |
| Böhler EMK 6 | G3Si1 | ER70S-6 | ~0.90 % | Mild steel, general purpose |
Technical characteristics and mechanical properties of the AUTROD 12.51 wire
The ESAB AUTROD 12.51 is a mild steel solid wire designed for MIG/MAG welding under shielding gas. Its chemical composition is carefully controlled to ensure regular beads and excellent mechanical strength.
It is manufactured in accordance with EN ISO 14341-A (G 42 2 C/M G2Si1) and AWS A5.18 (ER70S-3) standards. These classifications ensure broad compatibility with common structural steels.
The wire is available in standard diameters: 0.8 mm, 1.0 mm, and 1.2 mm. Each diameter covers different sheet thicknesses and welding intensities.
Mechanical properties of the deposited metal (typical values):
- Tensile strength: ≥ 500 MPa
- Yield strength: ≥ 420 MPa
- Elongation at break: ≥ 22 %
- Impact toughness KV at -20 °C: ≥ 47 J
The copper coating on the wire limits contact resistance and reduces contact tip wear. Feeding is smooth, even at high speeds.
| Product | Standard | Recommended Gas | Si Content | Typical Usage |
|---|---|---|---|---|
| ESAB AUTROD 12.51 | G 42 2 C/M G2Si1 / ER70S-3 | Pure CO₂ or Ar/CO₂ | ~0.65 % | Mild steel, general construction |
| ESAB AUTROD 12.64 | G 46 4 M G3Si1 / ER70S-6 | Ar/CO₂ (M21) | ~0.85 % | Slightly oxidized mild steel, less clean surfaces |
| Lincoln Electric SuperArc L-56 | ER70S-6 | Ar/CO₂ (M21) | ~0.85 % | Mild steel, oxidized or rusted surfaces |
| Böhler EMK 6 | G 42 4 M G3Si1 / ER70S-6 | Ar/CO₂ (M21) | ~0.80 % | Mild steel, all-position semi-auto welding |
The AUTROD 12.51 stands out for its moderate silicon content. It is perfectly suited for clean and well-prepared steels, where an ER70S-6 wire might provide more slag than necessary.
Fields of application: which materials and processes are compatible?
The ESAB AUTROD 12.51 MIG wire is designed for MIG/MAG welding of non-alloy and low-alloy steels. It is perfectly suited for common mild steels, in particular grades S235, S275, and S355.
This solid wire can be used both with direct current reverse polarity (DC+) and with conventional shielding gases. It is compatible with Ar/CO₂ mixtures (typically 82/18 or 75/25) as well as pure CO₂.
Sectors that use it daily:
- Boilermaking and light to heavy steel construction
- Fabrication of welded structures and frames
- Automotive industry and bodywork
- Industrial maintenance and repair
- Low-pressure steel piping
Recommended welding parameters
Settings vary according to the wire diameter used. Here are the common ranges for the most popular diameters:
| Diameter (mm) | Current (A) | Voltage (V) | Recommended Gas | Welding Position |
|---|---|---|---|---|
| 0.8 | 60-180 | 16-22 | Ar/CO₂ or pure CO₂ | All positions |
| 1.0 | 80-250 | 17-26 | Ar/CO₂ or pure CO₂ | All positions |
| 1.2 | 120-350 | 19-30 | Ar/CO₂ or pure CO₂ | PA, PB, PC |
| 1.6 | 200-500 | 22-34 | Ar/CO₂ or pure CO₂ | PA, PB |
In 1.2 mm diameter with an Ar/CO₂ mixture, the AUTROD 12.51 offers a very stable arc and excellent spray transfer at high intensity. This is the preferred setting for filling passes on thick plates.
For work in difficult positions (vertical up, overhead), prefer the 0.8 or 1.0 mm diameter with short-circuiting mode to control the weld pool.
Comparison: ESAB AUTROD 12.51 versus other mild steel MIG wires on the market
The market for mild steel MIG wires is broad. To help clarify, here is how the ESAB AUTROD 12.51 compares to the most well-known references.
The 12.51 is an ER70S-6 solid wire, the most popular for MIG/MAG welding on non-alloy steels. Its high manganese and silicon content gives it an advantage on slightly oxidized or greasy surfaces, where other wires fail.
| Product | Manufacturer | Classification | Si/Mn Content | Strength | Typical Usage |
|---|---|---|---|---|---|
| AUTROD 12.51 | ESAB | ER70S-6 / G3Si1 | High | Excellent tolerance to imperfect surfaces, stable arc | Steel construction, light boilermaking |
| AUTROD 12.22 | ESAB | ER70S-3 / G2Si | Moderate | Less slag, welding on clean steel | Pickled steels, clean surfaces |
| Filarc PZ6500 | ESAB | ER70S-6 | High | Optimized for high-speed robotic welding | Automotive industry, mass production |
| Marathon Pac 12.51 | ESAB | ER70S-6 / G3Si1 | High | Same filler metal, giant spool packaging for robots | Automated welding, continuous production |
| Lincoln SuperArc L-56 | Lincoln Electric | ER70S-6 | High | Soft arc, good penetration | Repair, general fabrication |
| Böhler EMK 6 | Voestalpine Böhler | ER70S-6 / G3Si1 | High | Very low spatter level | Fine boilermaking, visible welding |
Compared to its direct competitors in ER70S-6, the AUTROD 12.51 is distinguished by the consistency of its manufacturing quality and the regularity of its diameter from wire to wire, a crucial point for arc stability in production.
Compared to the AUTROD 12.22 (G2Si), the 12.51 better tolerates less well-prepared steels. If your surface is clean and pickled, the 12.22 generates less slag. For everything else, the 12.51 is the default choice.
Usage tips and best practices to optimize your welds
The ESAB AUTROD 12.51 MIG wire gives its best performance when machine settings and part preparation are carefully managed. Here are the key points to respect.
Prepare your parts before welding. Degrease and pickle the surfaces to be joined. Oxides, rust, or oil residues degrade bead quality and generate porosity.
Use an appropriate shielding gas: an Ar/CO₂ (80/20) mixture is suitable for most mild steel applications. Pure CO₂ remains an economical option but produces more spatter.
Set the gas flow between 12 and 18 L/min. Flow that is too low exposes the weld pool to ambient air; flow that is too high creates turbulence and impairs protection.
Adapt the wire feed speed and intensity to the part's thickness. On thin sheets (1 to 2 mm), reduce the voltage to avoid burn-through. On thicknesses greater than 6 mm, favor multiple passes.
Maintain a torch angle between 10° and 15° relative to the vertical and a regular contact-tip-to-work distance (stick-out of 10 to 15 mm). This stabilizes the arc and improves penetration.
Regularly clean the wire liner and check the condition of the drive rolls. Poorly guided wire causes arc stuttering and fusion defects.
FAQ - ESAB AUTROD 12.51 MIG WIRE
1. What types of steel is the ESAB AUTROD 12.51 wire suitable for?
The AUTROD 12.51 is designed to weld mild steels and non-alloy structural steels.
It is perfectly suited for S235, S275, and S355 type steels, which are very common in boilermaking, metalworking, and mechanical construction.
2. Which shielding gas should be used with this MIG wire?
The AUTROD 12.51 works with an Ar/CO₂ mixture (typically M21: 80% argon / 20% CO₂).
Pure CO₂ (C1) can also be used. It provides deeper penetration but generates more spatter.
For a clean weld with little spatter, the Ar/CO₂ mixture remains the best option.
3. What is the difference between the AUTROD 12.51 and the AUTROD 12.10?
The AUTROD 12.10 is a basic, economical wire for common applications without high mechanical requirements.
The AUTROD 12.51 offers a higher manganese and silicon content, which improves the mechanical strength of the deposit and the quality of the weld pool.
For mechanically loaded assemblies, the AUTROD 12.51 is clearly the better choice.
4. Is this wire suitable for welding in all positions?
Yes. The AUTROD 12.51 can be used in all welding positions (PA, PB, PC, PF…).
Its pool fluidity and good deoxidation make it easier to work in vertical up or overhead positions.
5. Which standard covers the AUTROD 12.51?
This wire is classified according to standard EN ISO 14341: G 42 4 M21 3Si1.
It also meets the AWS A5.18 classification: ER70S-6, an international reference widely used to validate welding procedures (WPS/PQR).
6. Can the AUTROD 12.51 be used on slightly oxidized or rusted parts?
The AUTROD 12.51 contains sufficient deoxidizers (Si + Mn) to tolerate imperfect surface conditions.
However, it is still recommended to brush and degrease the parts before welding to ensure the mechanical quality of the joint.
For heavily degraded surfaces, prior pickling is required regardless of wire quality.
Quick order
All product references. Indicate your quantities and add everything to the cart at once.
| Ref. | Diameter | Packaging | Availability | Price | Quantity | |
|---|---|---|---|---|---|---|
| 1 / 5 kg | ESAB_1251104600 | 1 | 5 kg | On order | €38,80 | |
| 1 / 18 kg | ESAB_1251106710 | 1 | 18 kg | In stock | €97,80 | |
| 1.2 / 5 kg | ESAB_1251124600 | 1.2 | 5 kg | On order | €38,38 | |
| 1.2 / 18 kg | ESAB_1251126710 | 1.2 | 18 kg | In stock | €95,53 |
Taxes included. Discounts and shipping calculated at checkout.
Need some advice?
Unsure about the part number or quantity? Our technicians are available to answer your questions at 04 50 52 70 89, and we will provide a quote for your bulk orders within 24 hours.
- Quote within 24 hours
- Dedicated professional rates
- Technical advice by phone
Frequently Asked Questions
Any other questions?
Call us at +33 4 50 52 70 89 or write to contact@dagobertindustrie.com.
What are the shipping costs and delivery times?
In-stock items are delivered in 48-72 hours. Made-to-order items are delivered within 2 to 3 weeks. DPD delivery costs €5.95 incl. VAT and is free on purchases of €49 incl. VAT or more.
How to choose the right reference?
The specifications for each reference are detailed in the data sheet and the quick order table. If in doubt, call us at 04 50 52 70 89: we will guide you to the reference suited to your application.
Can I order several items at once?
Yes: the quick order pad lists all the references. Enter a quantity for each one, then add them all to your cart in one click.
I am a professional, can I get a quote?
Yes, write to us at contact@dagobertindustrie.com: response within 24 hours. The pro account gives you access to your net prices excluding tax.
Can I return a product?
Private customers have 14 days from receipt to withdraw. The product must be new, complete, and in its original packaging. Consult our refund policy.
Is the payment secure?
Yes. Payment is encrypted by our payment provider: we never have access to your bank details.
Discover the ESAB range
-
ESAB Sentinel A70 PRO Welding Helmet
Vendor:ESABRegular price €599,00TTCRegular price€499,17 HT -
ESAB Autrod 12.51 MIG Wire
Vendor:ESABRegular price From €38,38TTCRegular priceFrom €31,98 HT -
ESAB AristoRod 12.50 MIG Wire
Vendor:ESABRegular price From €39,59TTCRegular priceFrom €32,99 HT -
ESAB Rogue EMP 210 PRO Welding Machine
Vendor:ESABRegular price €1.499,00TTCRegular price€1.249,17 HT -
ESAB SENTINEL A60 WELDING HELMET
Vendor:ESABRegular price From €339,99TTCRegular priceFrom €283,33 HT


